Latest Program :
Recent Program
Showing posts with label G73. Show all posts

Longitudinal grooving compound fixed cycle


G73 Longitudinal grooving compound fixed cycle
          
[Command format]
          G73 X_ Z_ I_ K_ D_ L_ F_ E_ T_

         X: X coordinates of target point
          Z: Z coordinates of target point
          I: Shift distance in X-axis direction  (Diameter instruction.  If the instruction is not instructed, it is regarded as 0.)
          K: Shift distance in Z-axis direction  (If not instructed,   it is regarded as 0.)
          D: Cut depth
          L: Cut depth at removing the tool  (Diameter instruction)   (If not instructed, this sequence will not be executed.)
          DA: Instruct a return distance.  If DA is not instructed,  it is regarded as the return distance set to that of the  grooving, drill cycle (other function 1) of the optional   parameter.
          E: Dwell upon arrival at Z-axis target point (The unit of instruction is the same as G04.)  (If not instructed, this sequence will not be executed.)
          T: Tool compensation No. instruction which determines the tool compensation amount at Z-axis target point positioning (if not instructed, the T instruction at the start point positioning is used.  The T instruction next to this block, or the compensation number, acts as the T instruction at start point positioning.)
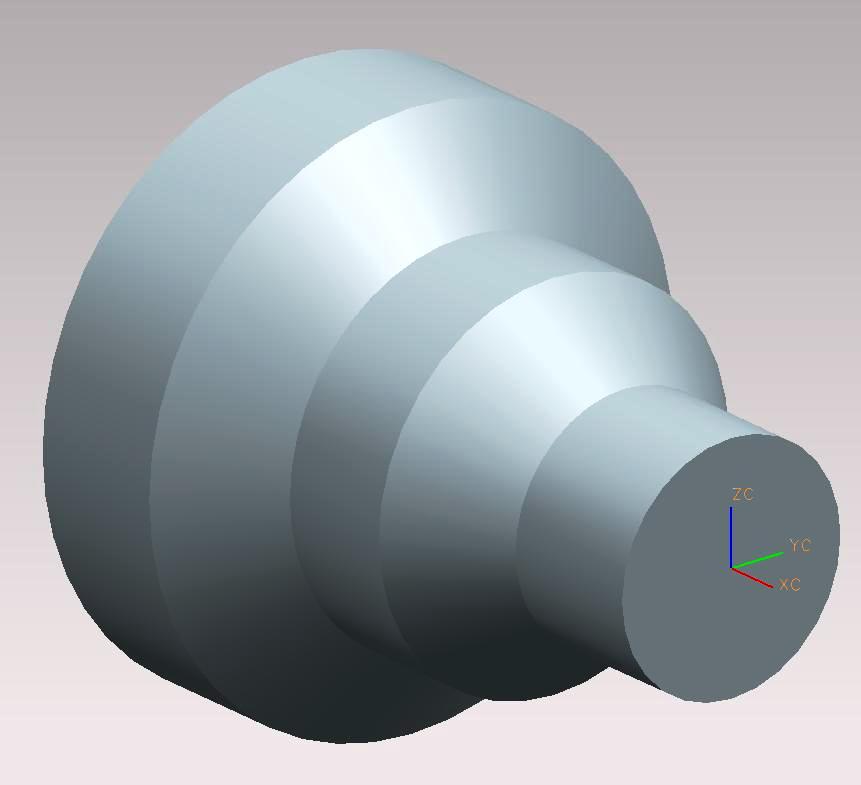
          

Contour –Parallel Roughing Cycle G73 Or Profile Turning Cycle Or Copy Turning Cycle

Contour –Parallel Roughing Cycle G73 Or Profile Turning Cycle Or Copy Turning Cycle


Profile Turning Cycle:-


          This function will allow efficient execution in roughing when cast or forged parts are to be cut along finish shape.


Programming Format:-


          G73 U___ W__ R__ ;
          G73 p__ Q__ U__ W__ F__ S__ T__ ;


          U       =        escape distance and direction in the X-axis direction ( radial value )


          W       =        escape distance and direction in the Z-axis direction


          R        =        times of divisions


          * Other Addresses Are As With G71


Tool Nose Radius Compensation:-


          When this cycle is commanded in the tool nose radius compensation mode, tool nose radius compensation is applied to the finishing shape sequence for this cycle and cycle is executed for this shape.
         
           However, when this cycle is commanded in the tool nose radius compensation mode, the compensation is temporarily cancelled immediately before this cycle and started at the head block of the finishing shape sequence.


Sample Program:-


N10     G00 G96 G98
N11     G28 U0 W0
N12     T0101
N13     X150. Z5.
N14     G73 U8. W6. R3.
N15     G73 P16 Q20 U4. W2. F150 S100 M3 ;
N16     G00 X50. ;
N17     G01 Z-30.;
N18     X80. Z-50. ;
N19     Z-75. ;
N20     X120. Z-90.0 ;
N21     G70 P16 Q20 ;
N22     G28 U0 W0 M5 ;
N23     M30 ;


Support : Creating Website | Johny Template | Mas Template
Copyright © 2011. Online Education - All Rights Reserved
Template Created by Creating Website Published by Mas Template
Proudly powered by Blogger